

 English
 中文简体
 русский


J.Parker: Successful Delivery & Commissioning of Combustion Systems for Southwest China’s Largest Sludge Incineration Plant
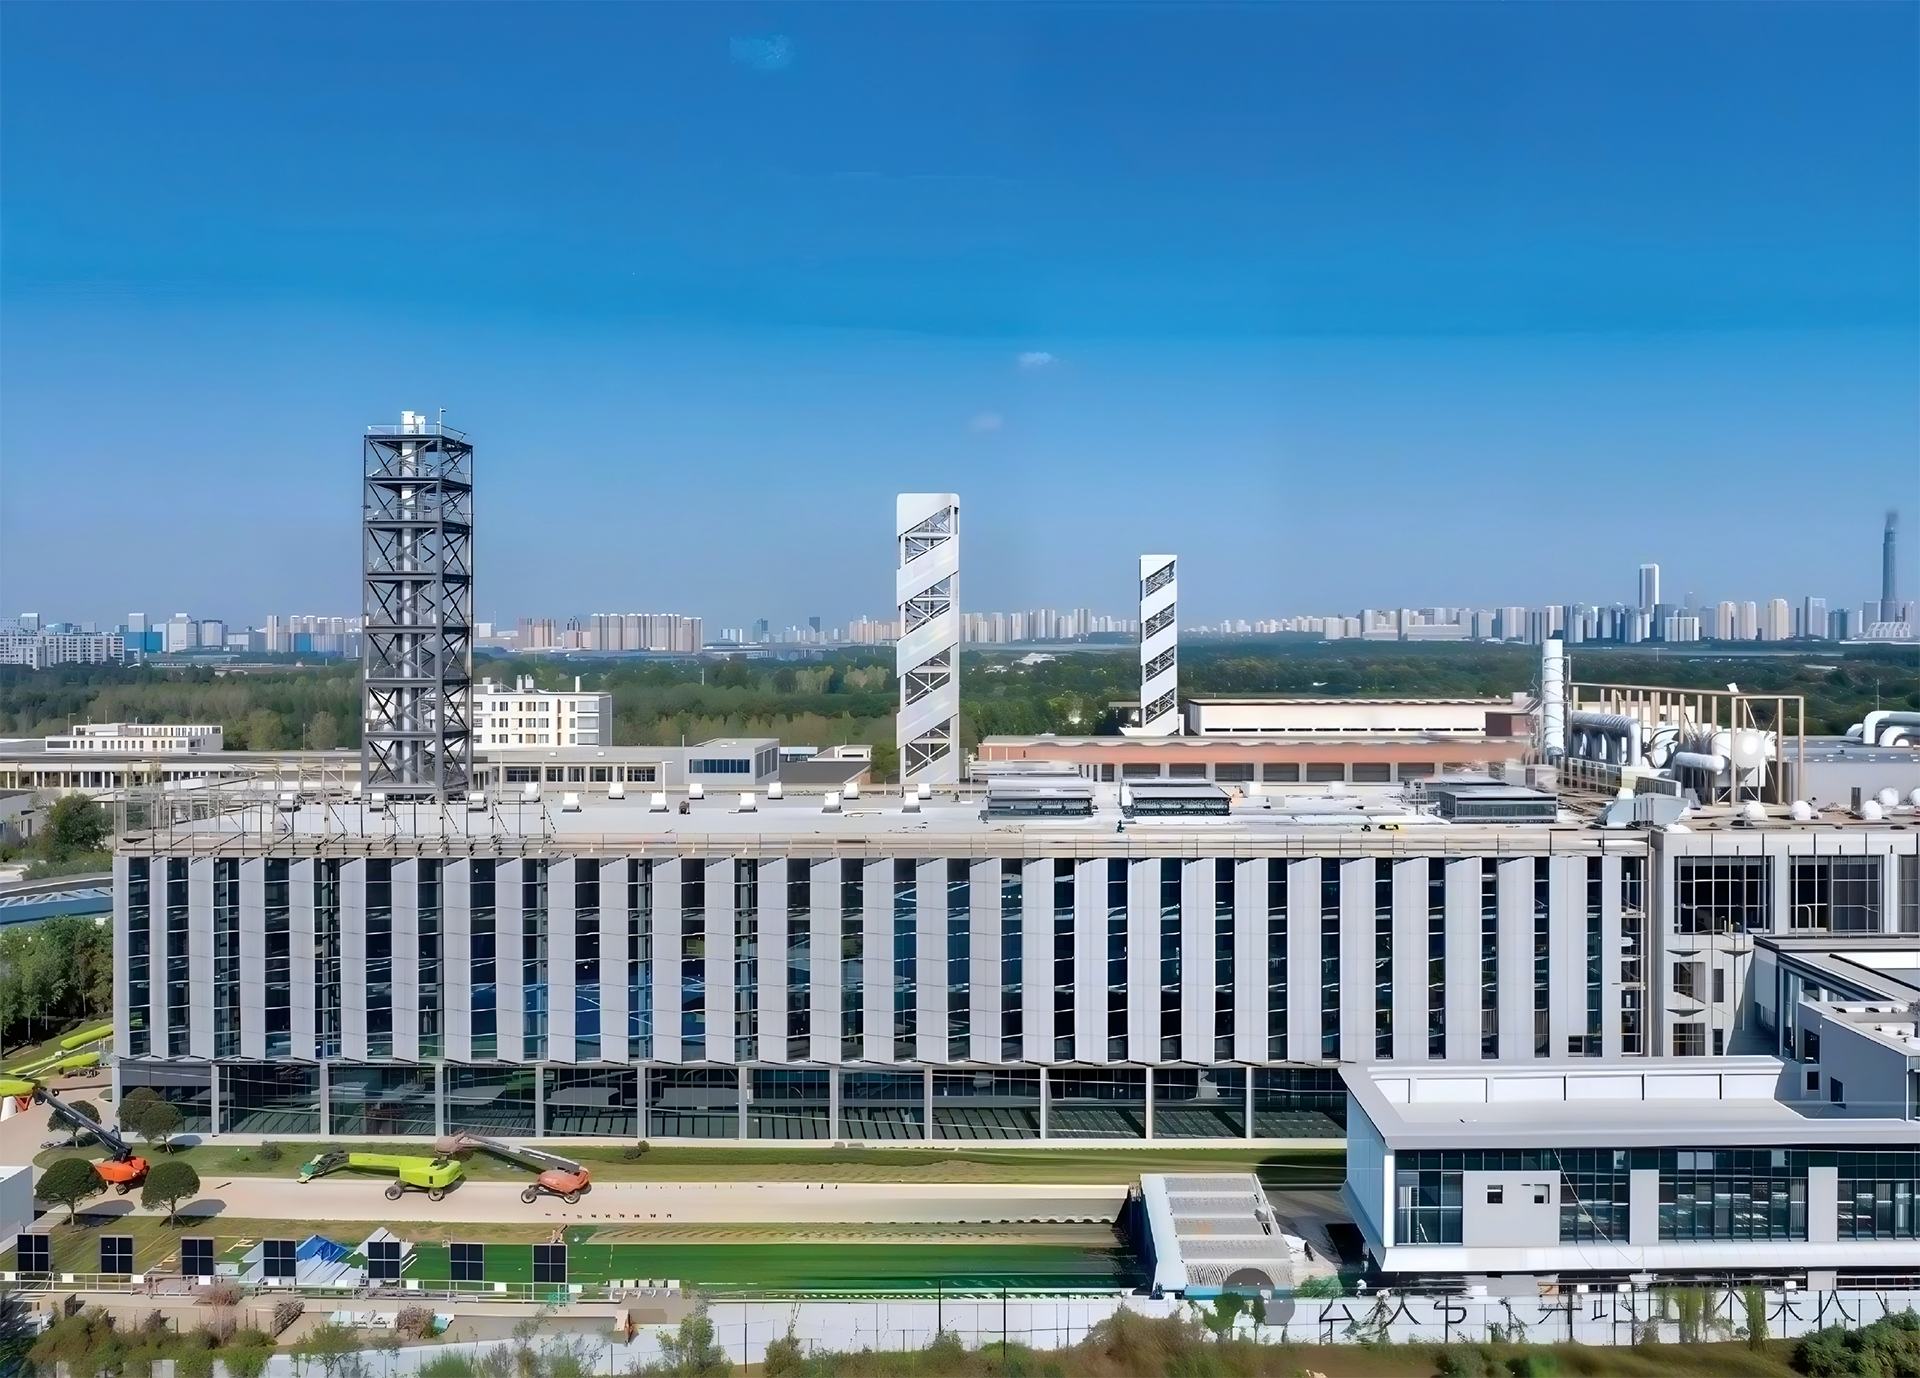
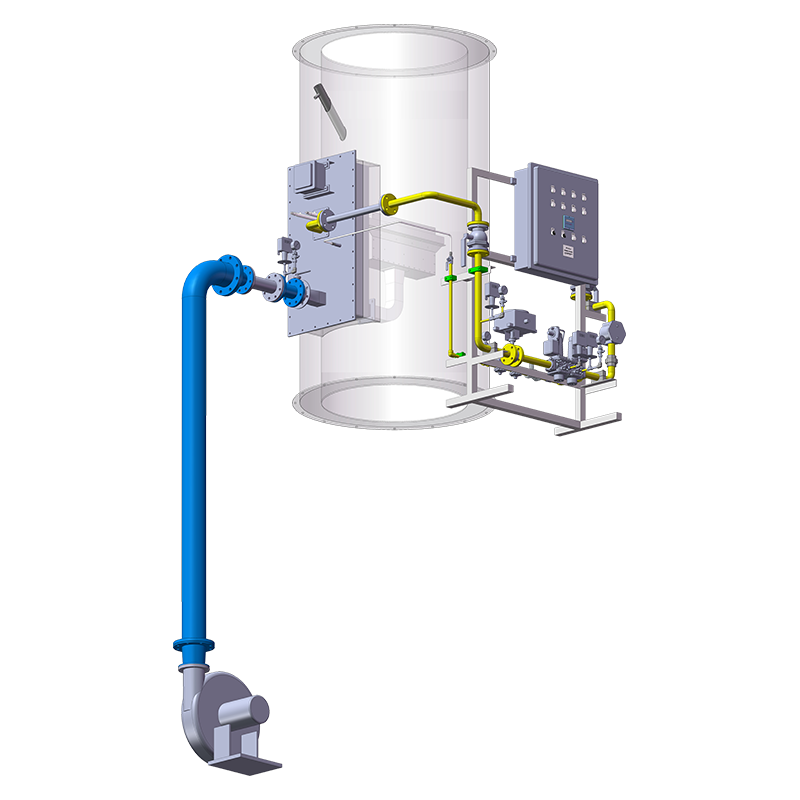
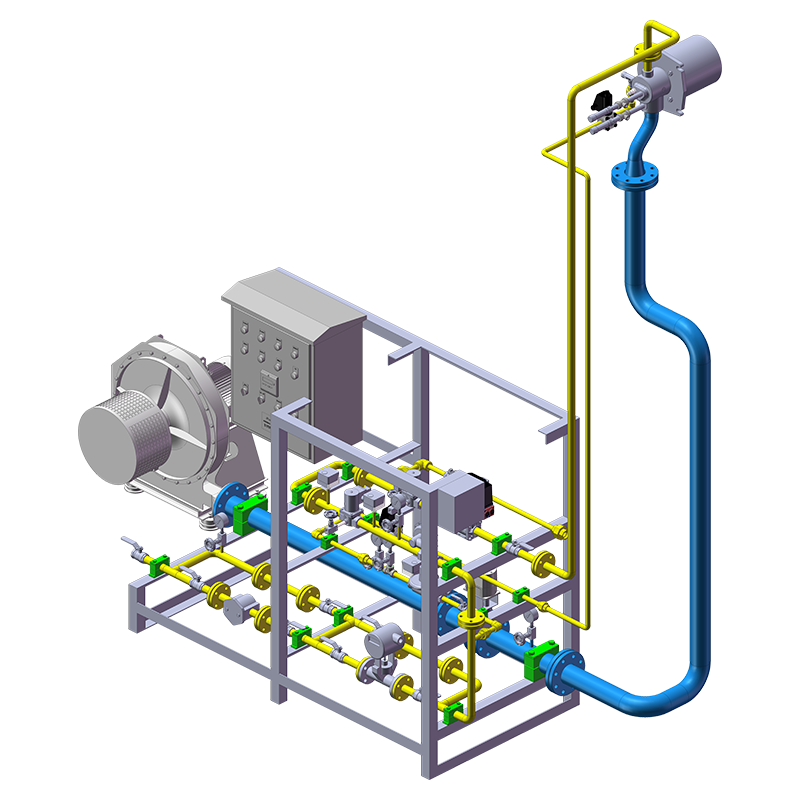
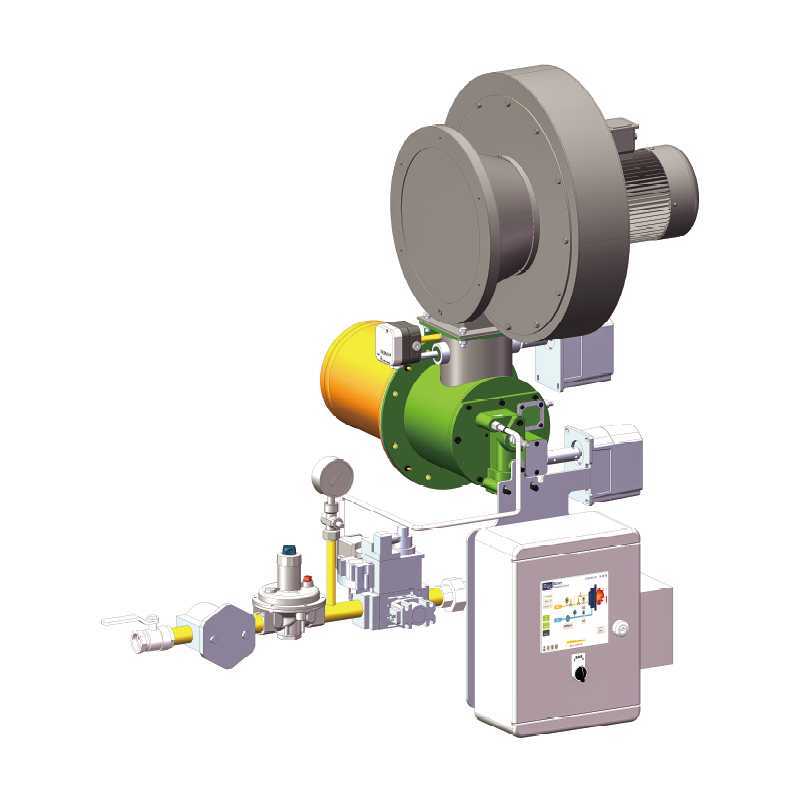
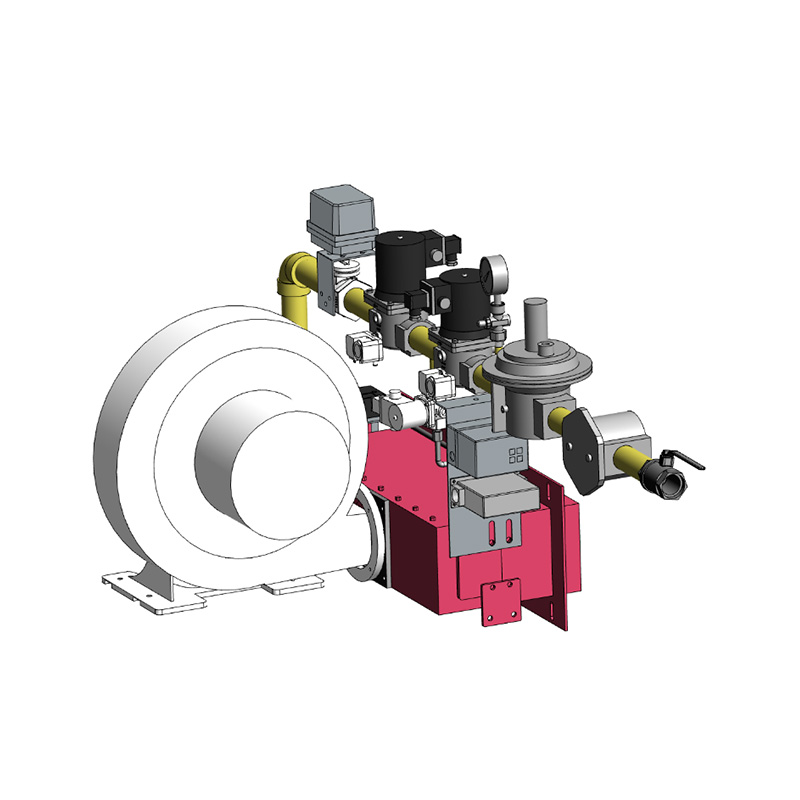
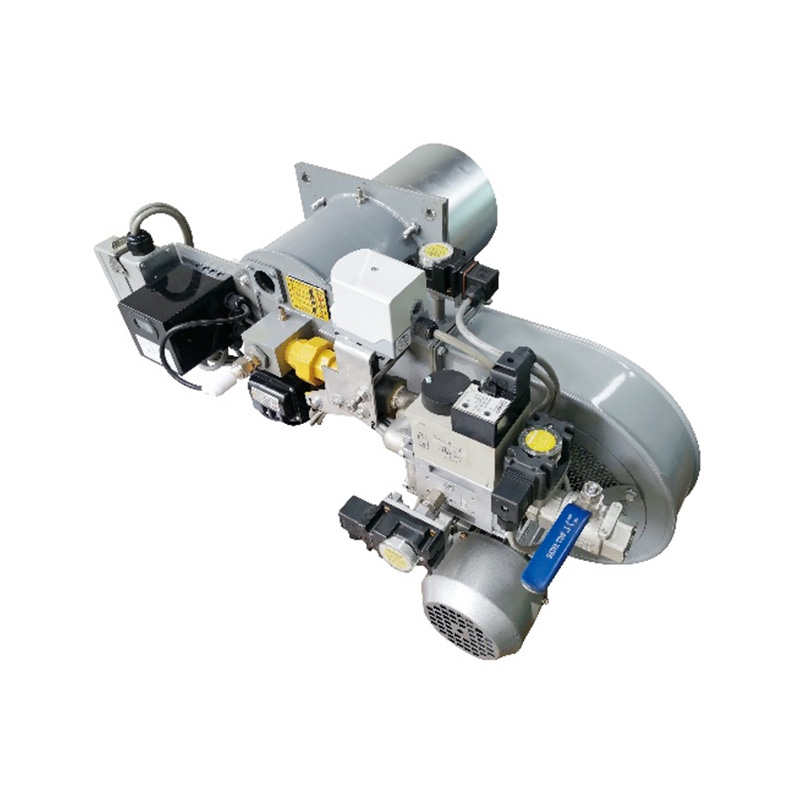
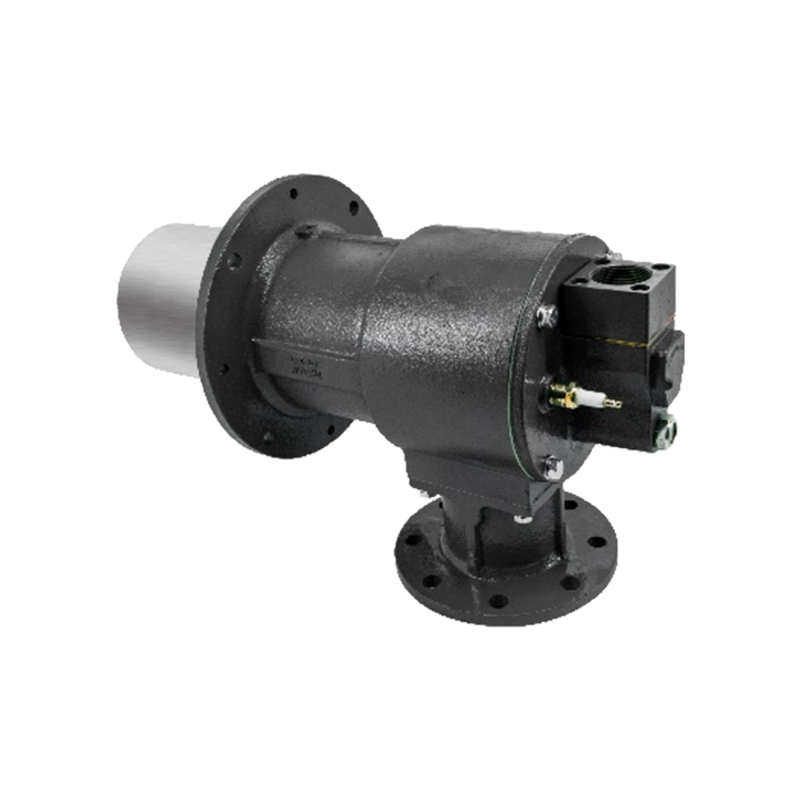
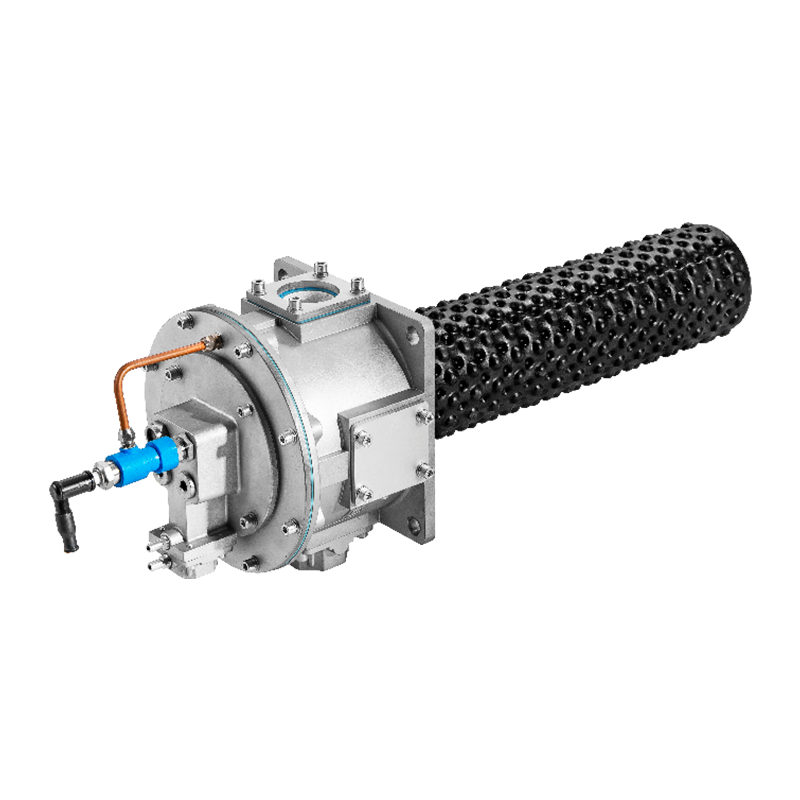
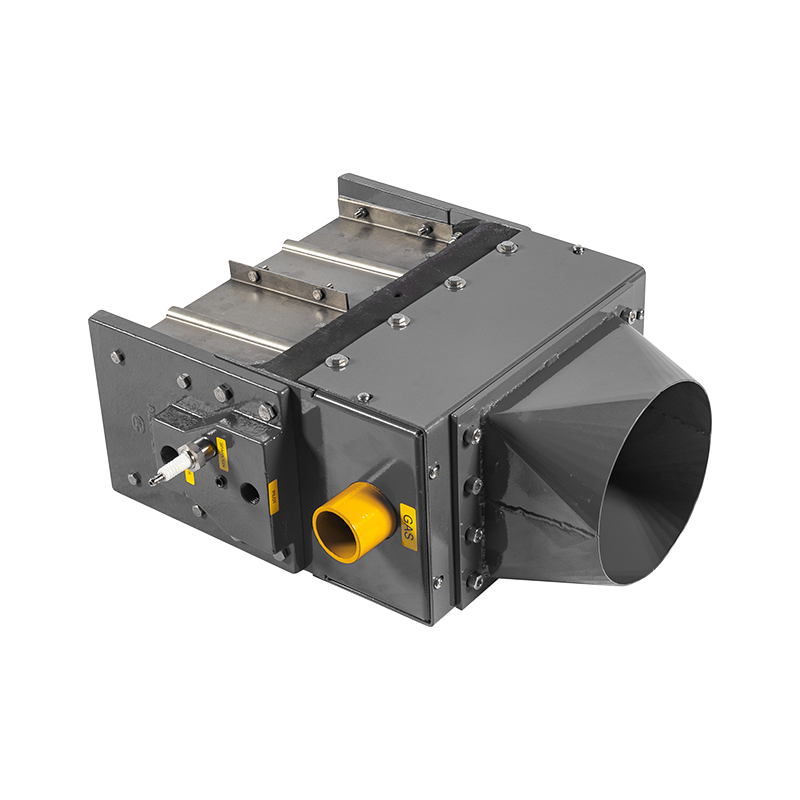
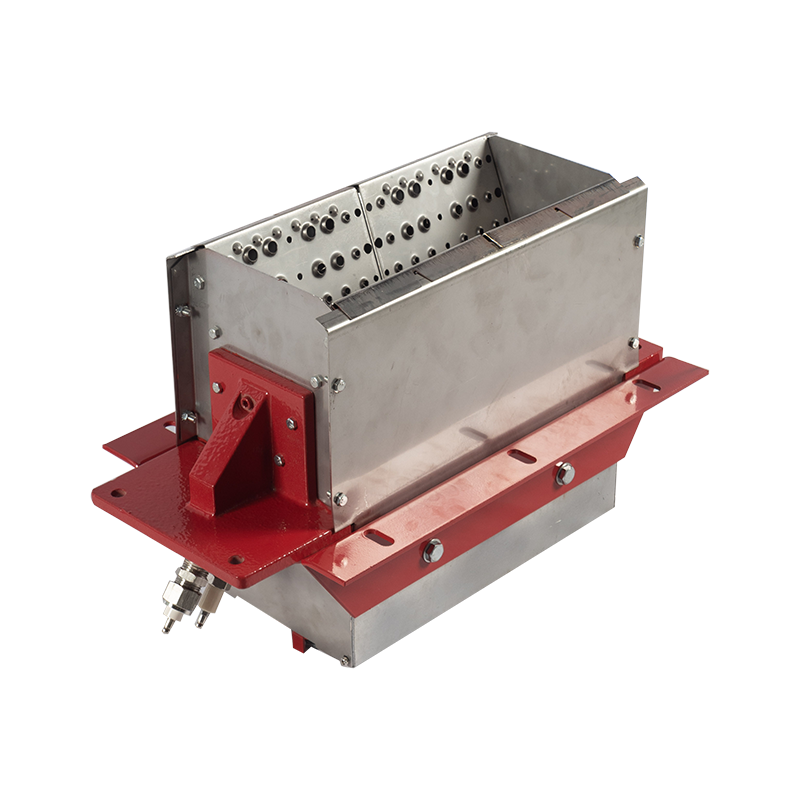
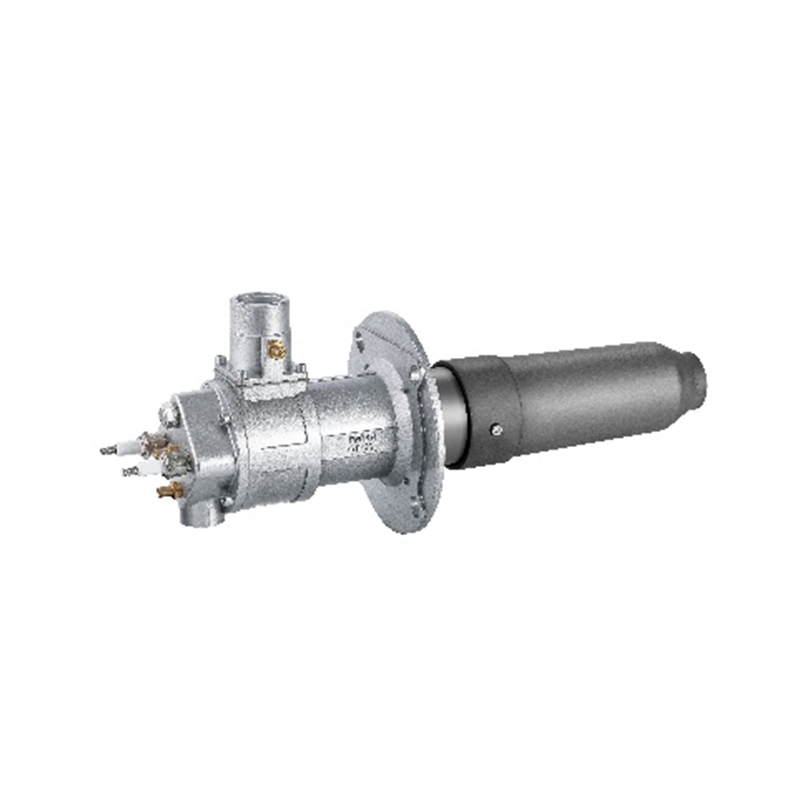
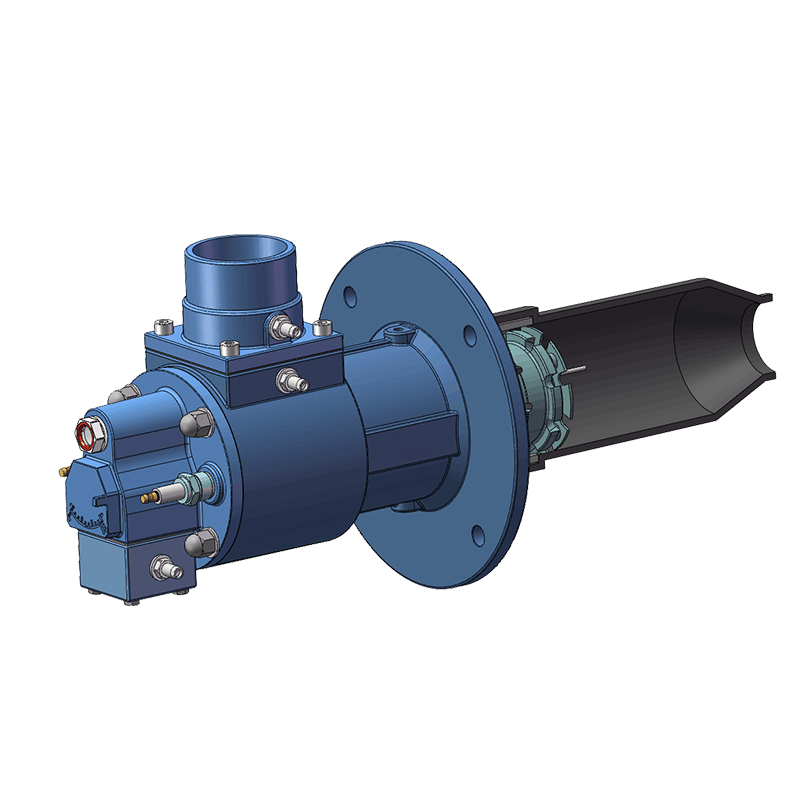
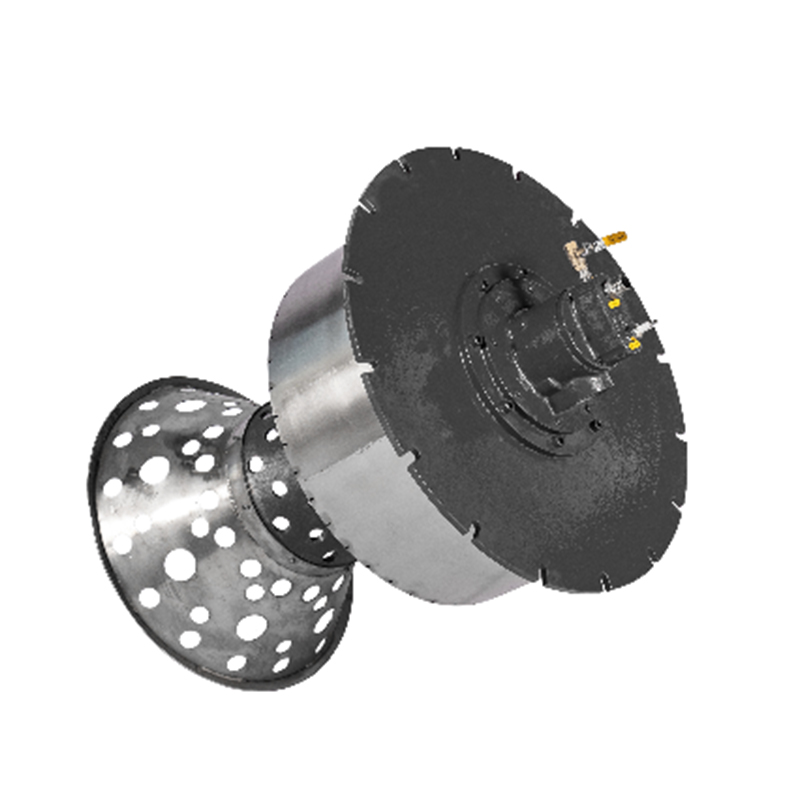
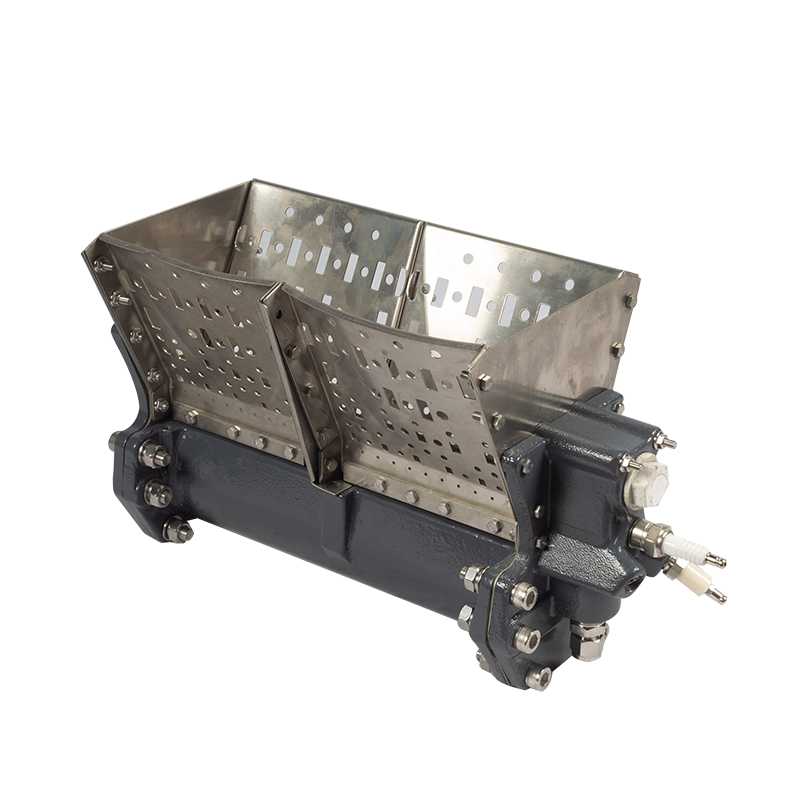
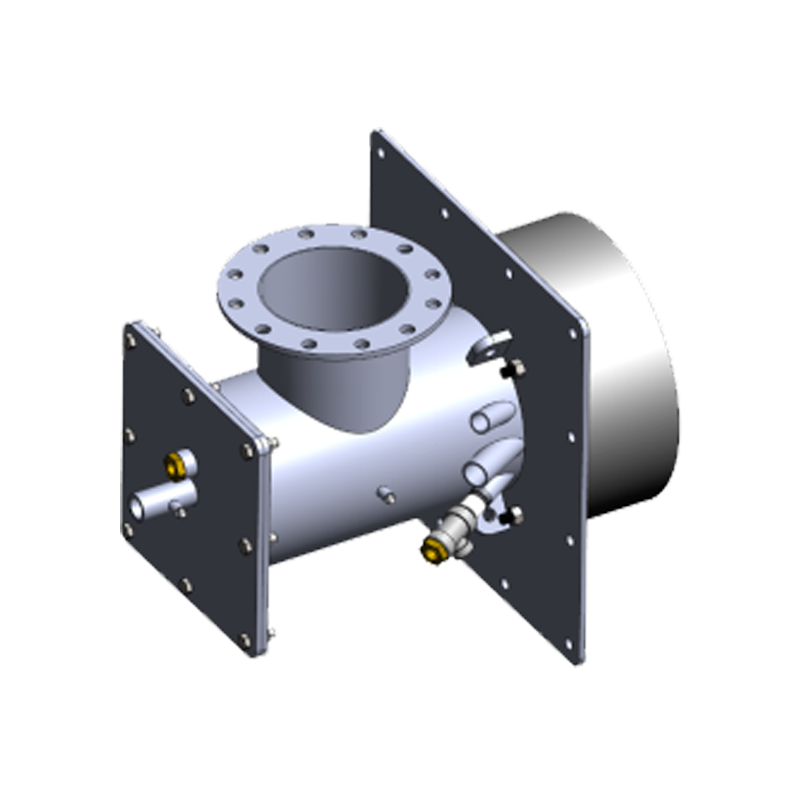
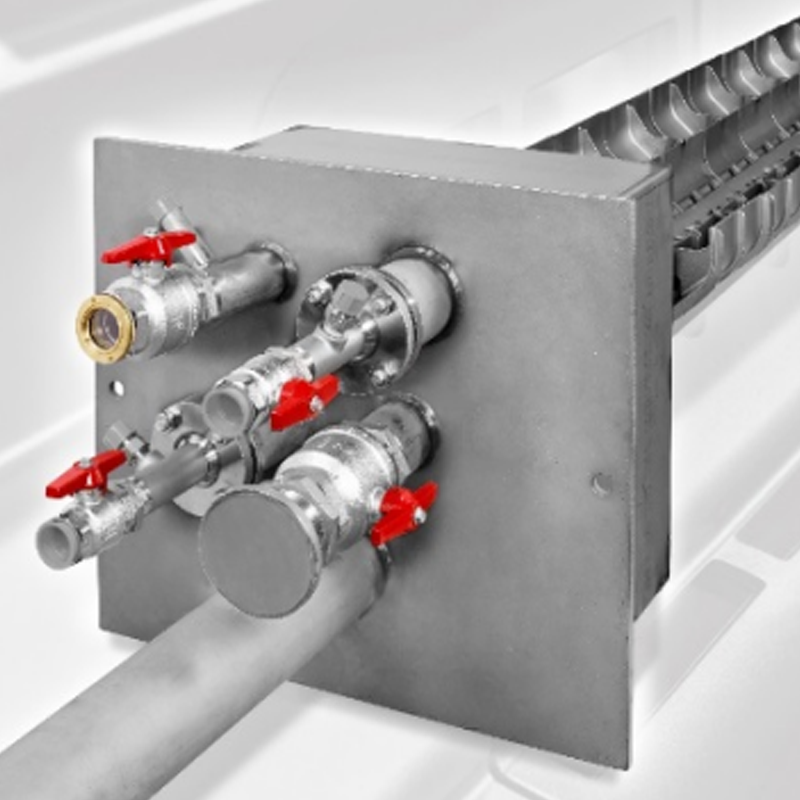
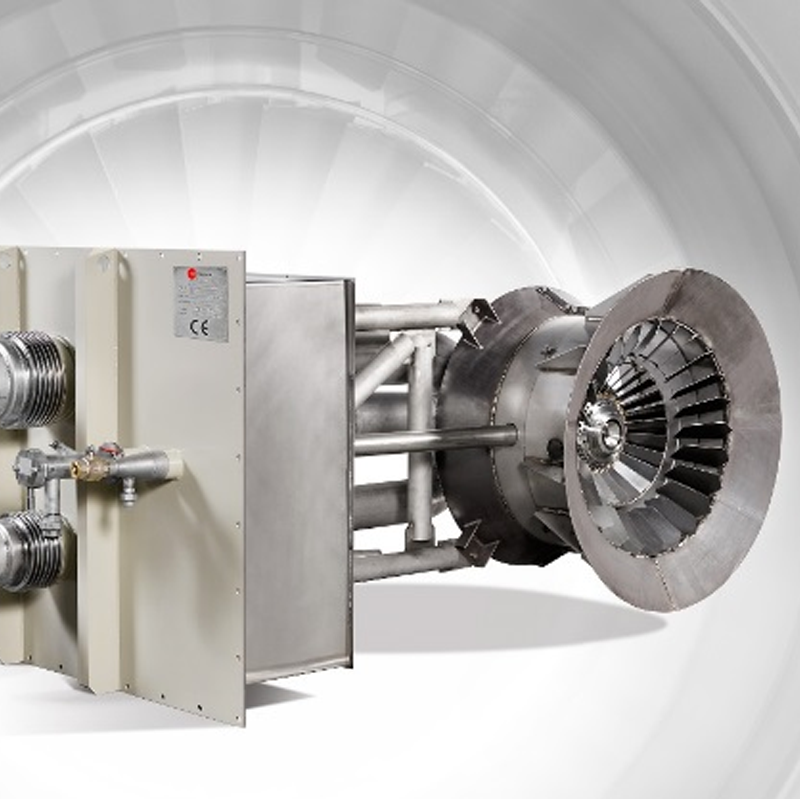
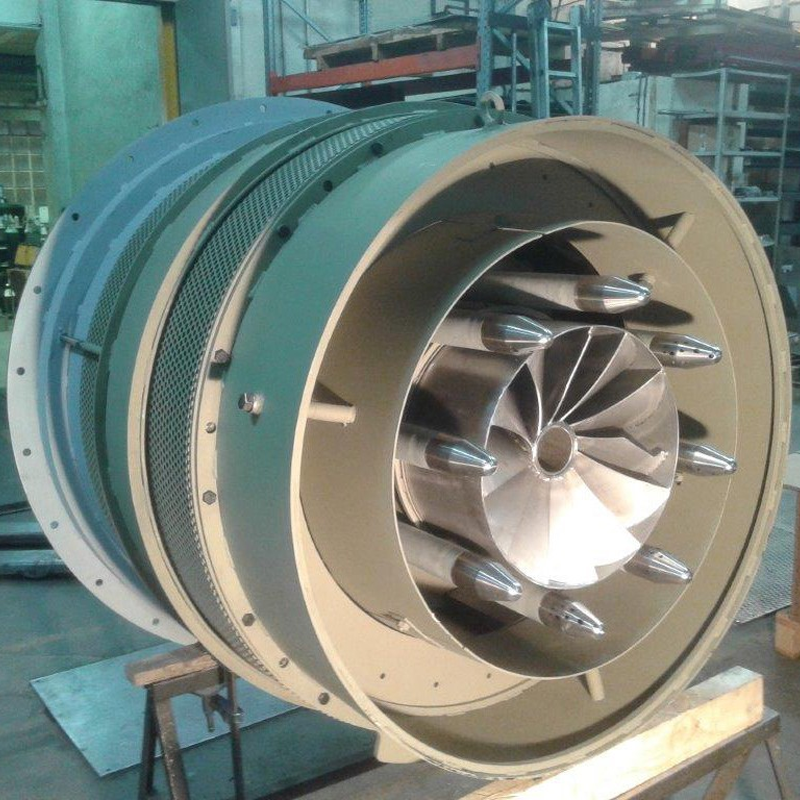
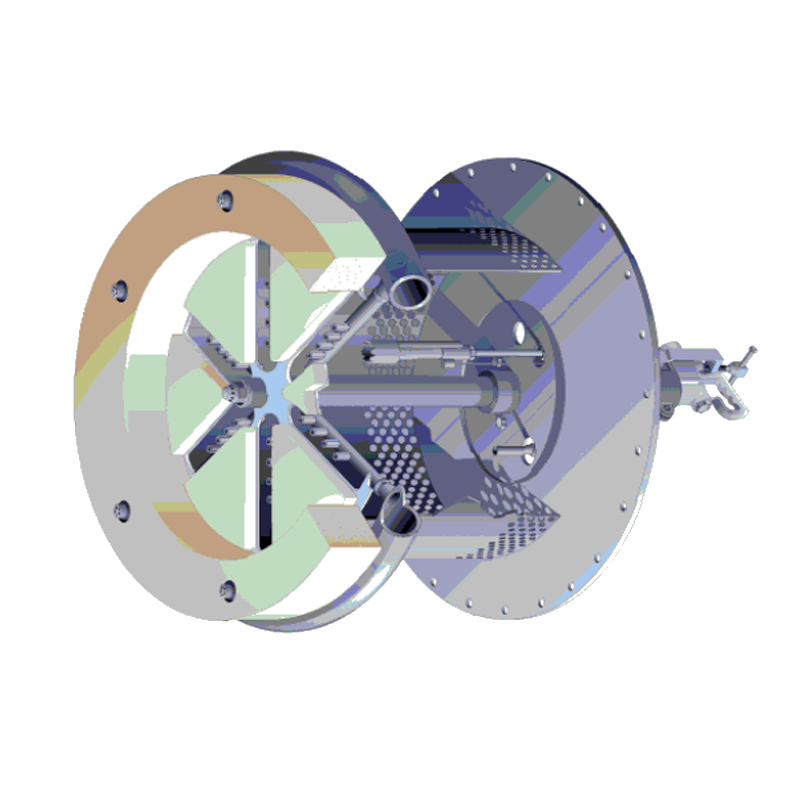
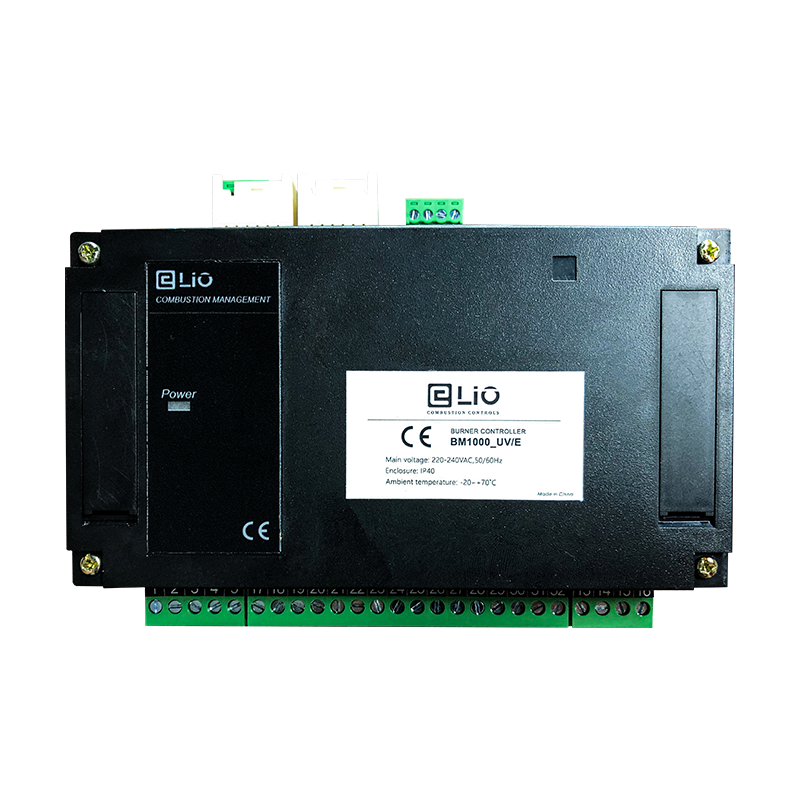
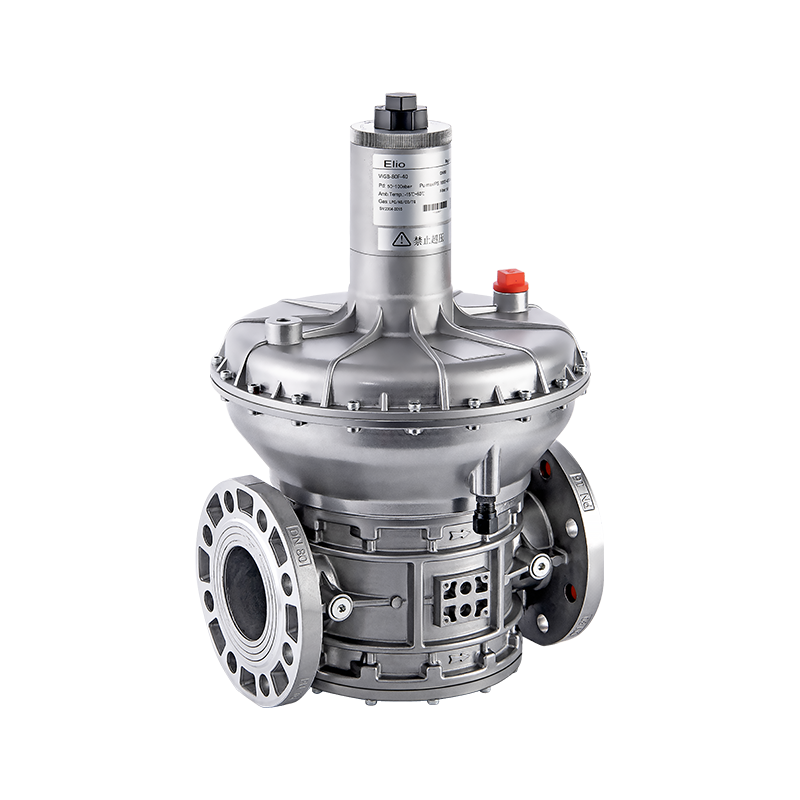
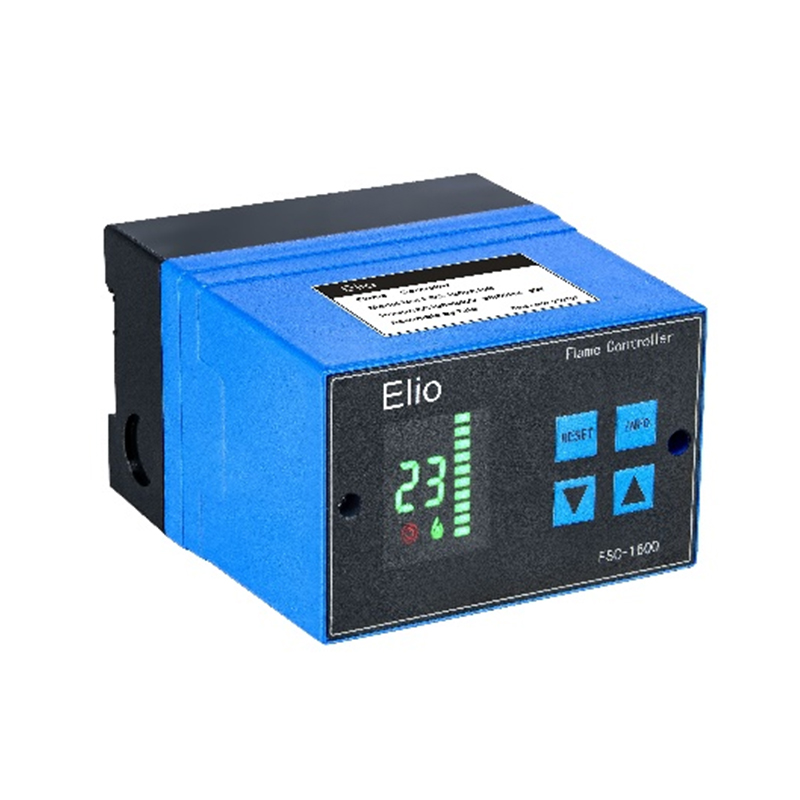
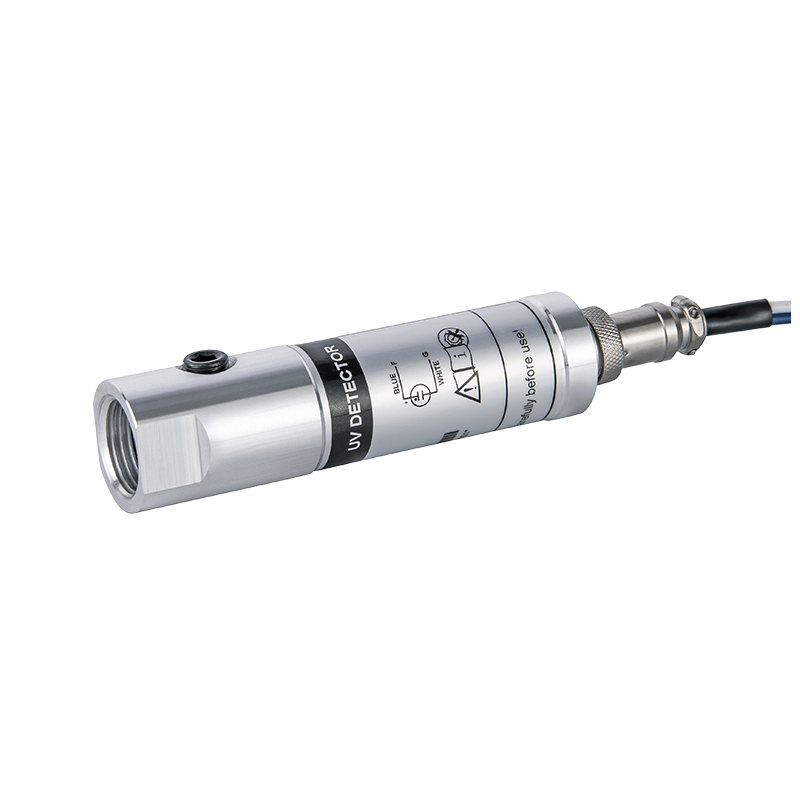
In November 2024, J.Parker completed the delivery and full commissioning of bespoke burner systems for a sludge incineration project in Chengdu. As the largest sludge incineration facility in southwest China, the plant is equipped with two production lines and features a designed processing capacity of 1,400 tons per day. J.Parker supplied a complete integrated combustion package for the Suez Thermylis fluid bed oxidizer, covering burners, gas train assemblies, and full burner management systems.
Following 18 months of uninterrupted operational deployment, the custom-engineered burner system has achieved excellent compatibility with the thermal oxidizer unit. The entire system maintains consistent and stable operation with zero unplanned shutdowns, smooth burner startup and shutdown cycles, and highly precise temperature regulation. Notably, the system delivers ultra-low CO and NOx emissions, exceeding the performance expectations of both the direct client Suez and the end-user.
I. Customized Combustion Solution for Thermylis Fluid Bed Oxidizer
J.Parker delivered a fully tailored combustion system adapted to the operational characteristics of the Suez Thermylis fluid bed oxidizer, with customized configurations for three core burner units as detailed below.
1. Preheating Burner System
Serving as the core equipment for cold furnace startup, the back-pressure-resistant gas-fired preheating burner is engineered with a maximum output of 5,500 kW and a 10:1 wide turndown ratio. It enables rapid heating of the incinerator from ambient temperature to the operational temperature of 850°C. During sand feeding operations, the furnace back pressure may surge to a maximum of 25kPa; the integrated furnace pressure compensation system dynamically adjusts in real time to sustain a constant air-fuel ratio and stable flame status.
The burner is structurally optimized for high back-pressure working conditions, supporting smooth and reliable restart under any fluctuating back-pressure scenarios to guarantee uninterrupted furnace preheating procedures.
2. Auxiliary Burner Fuel Injection System
The auxiliary burner system is configured to activate automatically once the furnace temperature reaches the temperature auto-ignition threshold. With a rated output of 5,200 kW and an extended 15:1 turndown ratio, the matching gas train ensures accurate and stable fuel injection under variable furnace back-pressure conditions. This design provides continuous supplementary thermal energy throughout the incineration process, underpinning consistent and efficient combustion stability.
3. Post-firing Burner System
The post-firing burner is rated at 2,400 kW with a 10:1 turndown ratio, specifically optimized for the unique operating parameters of the post-combustion zone. It adapts stably to furnace pressure ranging from -2 kPa to 3 kPa and excess air ratios between 10% and 50%.
This targeted configuration sustains high-efficiency, stable combustion in the post-firing section, maintaining the flue gas temperature steadily at 850°C without overheating. The design balances optimal thermal efficiency with thorough oxidation of harmful flue gas components, meeting strict environmental and operational standards.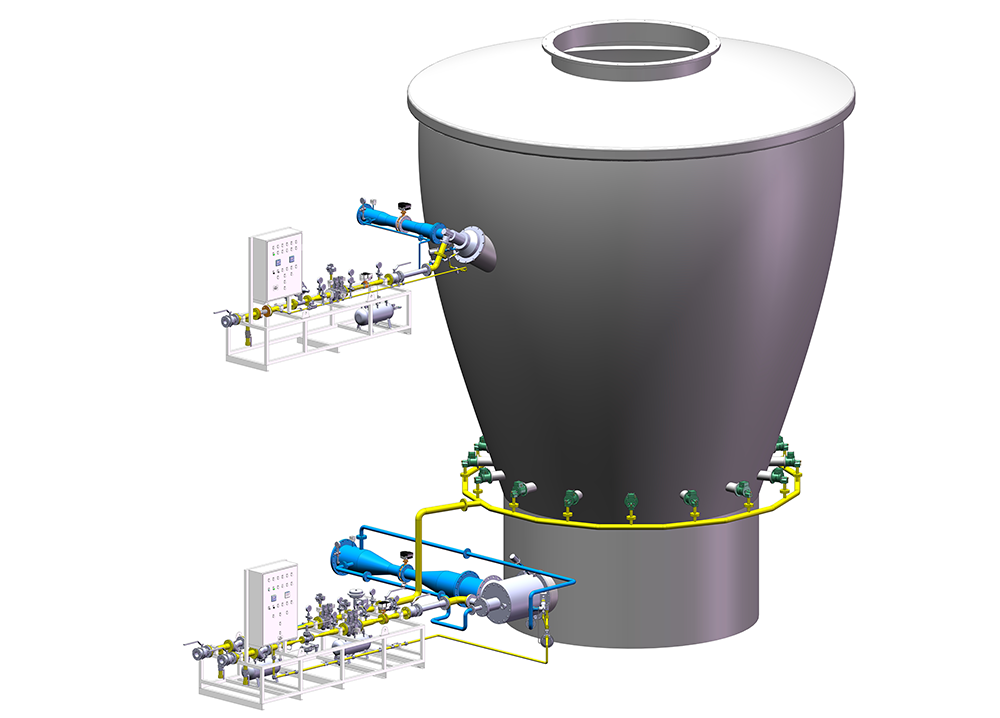
II. On-site Commissioning and Performance Verification
During the project commissioning phase, J.Parker’s professional after-sales technical team conducted systematic equipment testing, parameter calibration, and operational optimization in strict compliance with project technical specifications and industrial standards.
1. Single Burner Stability Test
A continuous 10-day single burner stability test was completed on-site. During the test, fluidized bed sand feeding was gradually implemented, with the wind chamber pressure rising to 14 kPa. Throughout the full test cycle, all burners maintained stable and reliable operation, fully verifying the system’s adaptability and operational stability under high-load and demanding process conditions.
2. System Joint Commissioning
In the joint commissioning stage, all burner units operated in precise synchronization with the full sludge incineration system. Equipped with intelligent temperature modulation and safety combustion control logic, the complete combustion system successfully passed a 168-hour continuous full-load operation test. The test comprehensively validated the superior system integration performance, operational stability and long-duration reliability of J.Parker’s customized combustion solution.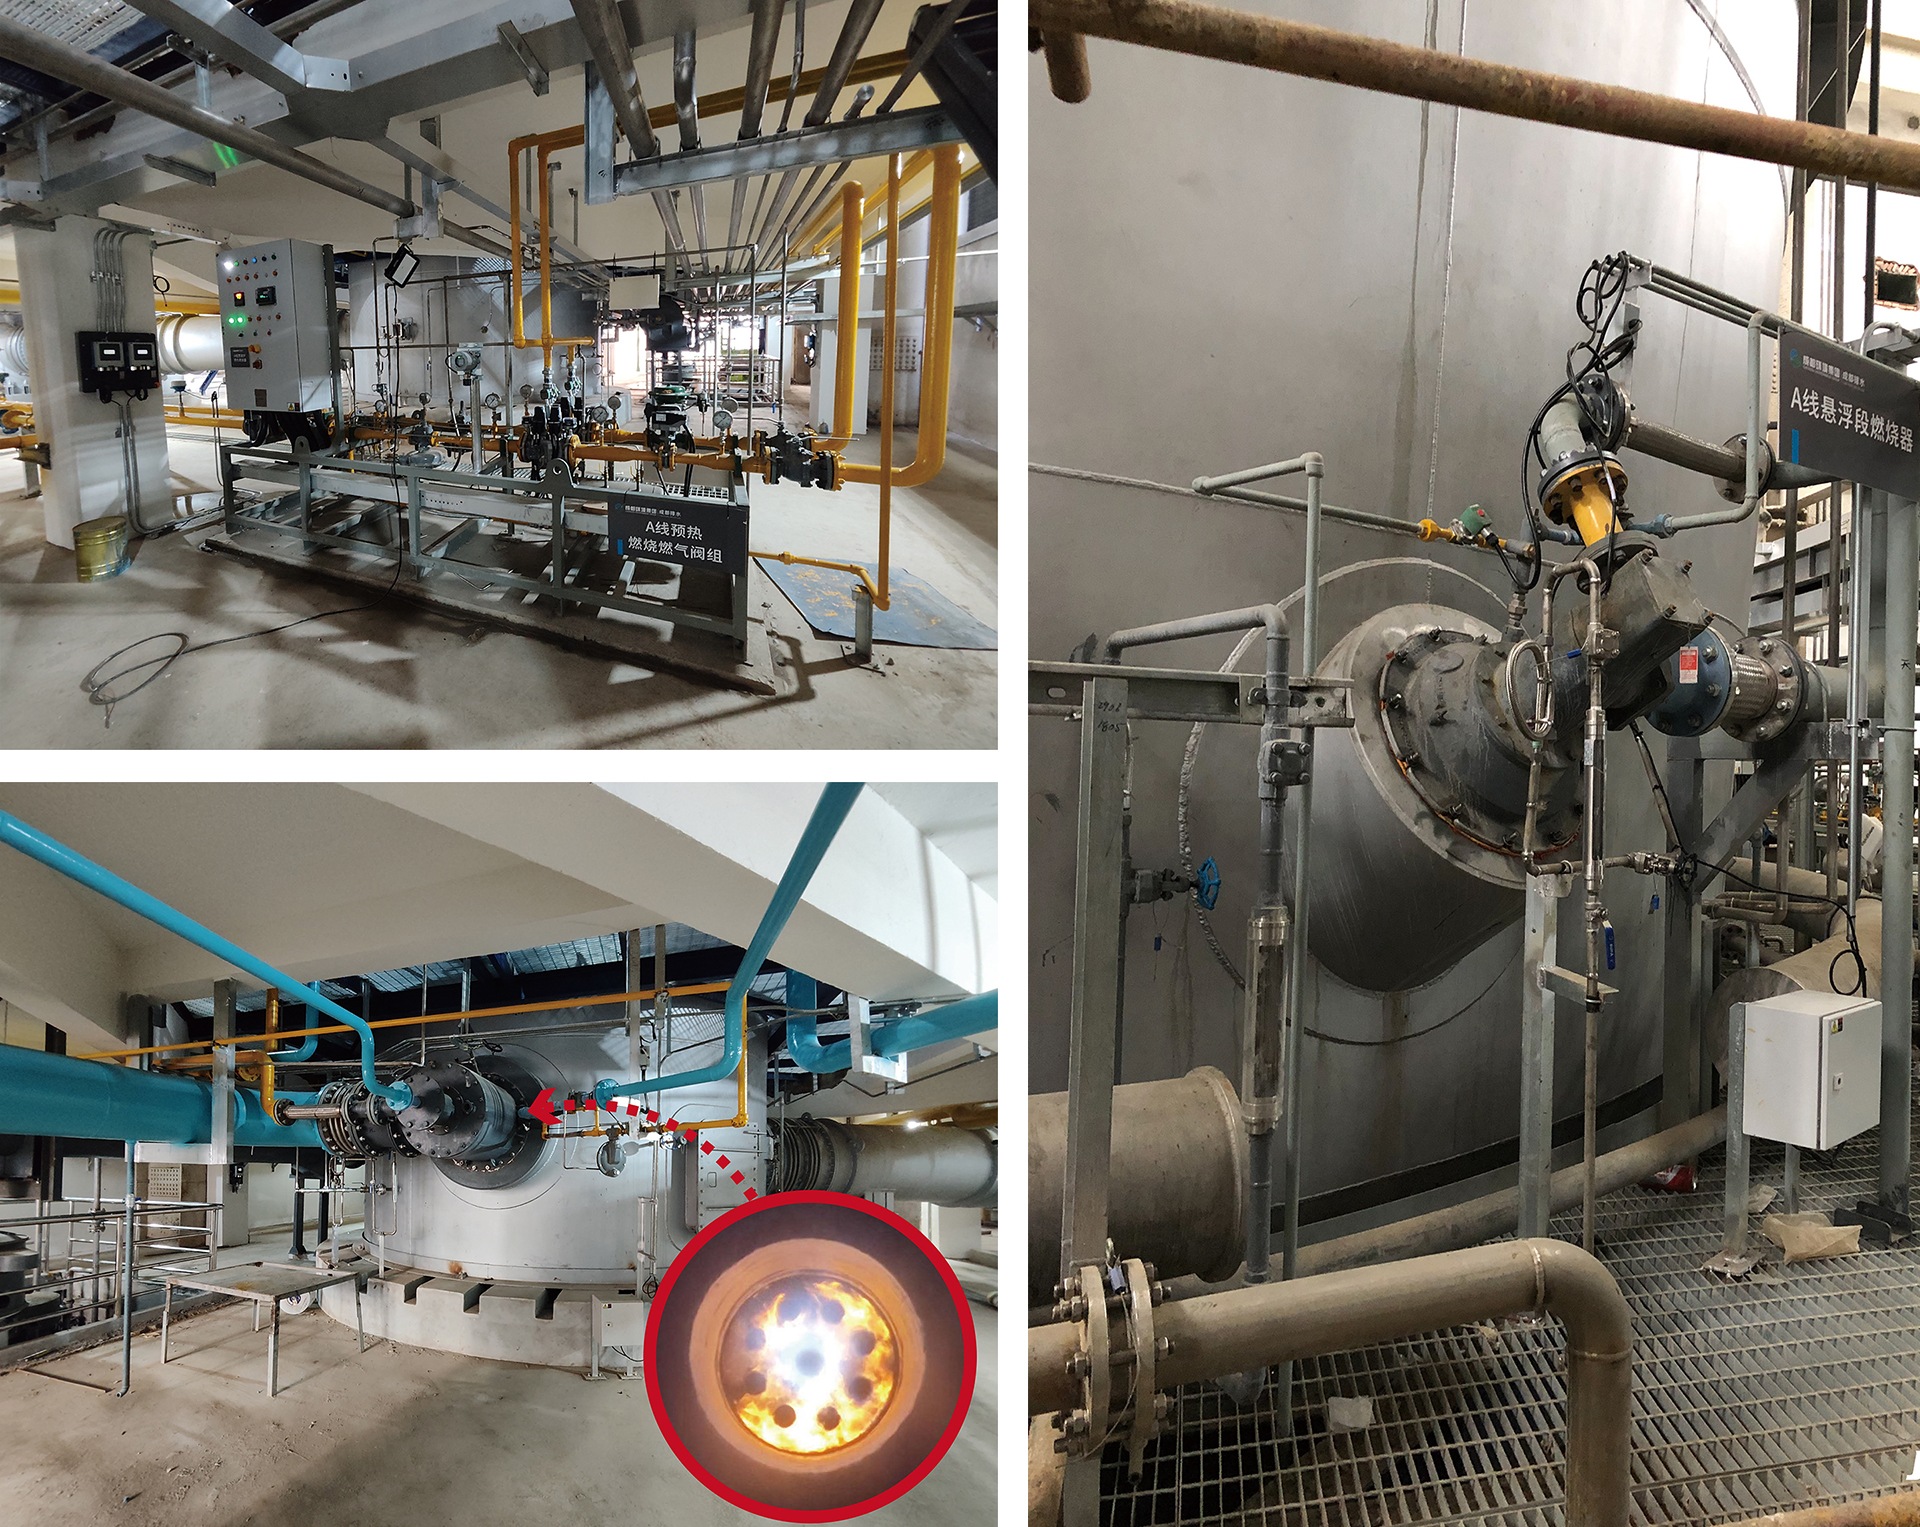
We are committed to the development of combustion systems, including combustion system design, manufacturing, sales andafter-sales service.
Product Category
Contact
- Phone: +86 183 2176 4313
- Tel: +86-21-5678-0598
- E-mail: [email protected]
- Address: 6# building of Gaochuang industry park, Yancheng, Jiangsu Province, China
Copyright © J. Parker Combustion Equipment (Jiangsu) Co., Ltd. All Rights Reserved
